If you’re a machinist, production supervisor, or small shop owner, you’ve probably stood in front of a shelf of cutting tools at some point, thinking: Does this bit actually work with my mill, lathe, or CNC machine? As someone who’s spent 12 years as a cutting tool supplier — troubleshooting compatibility missteps, walking shops through first-time tool installations, and even visiting small factories to fix a wrong-tool match that halted a $50,000 order — I can tell you this is one of the most common, costly mistakes in metalworking (and woodworking, for that matter). A wrong tool doesn’t just slow you down; it can scratch a precision part, damage a spindle, or waste hours of setup time. In this post, I’ll break down exactly how to verify compatibility, no guesswork required — and I’ll even throw in a few hard lessons I’ve learned from years on the job. Cutting Tool
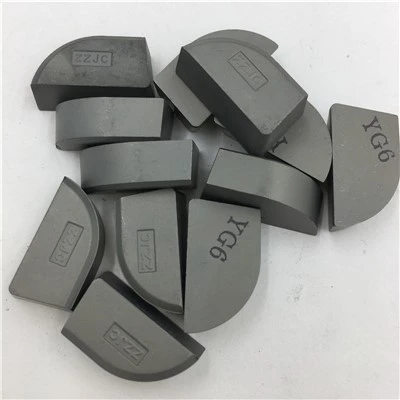
First, let’s get the basics out of the way: compatibility has less to do with the tool’s brand or price tag, and more about three core connections between your machine and your tool. I call these the “Three P’s”: Part Mounting, Performance Specs, and Process Requirements. Skip even one, and you’re risking a downtime headache. Let’s start with the first and most obvious: part mounting. This is the physical fit between your tool’s shank, arbor, or holder and your machine’s tool taper or spindle. I can’t tell you how many times a shop’s manager has called me panicking because they ordered a ¼-inch end mill only to find it’s too loose in their lathe collet. This is non-negotiable, so here’s how to measure it right.
First, pull up your machine’s manual. Yes, I know — half of us toss those the second the machine arrives, and the other half swear they’re “too old school” to reference them. Trust me, I’ve seen more than one $10,000 CNC mill sidelined because someone skipped checking the manual’s spindle taper size. For example, a standard 3-axis vertical mill might have an R8 taper, while many modern lathes use a Morse Taper #4 (MT4). If your tool’s shank doesn’t match that taper number, it won’t lock in — plain and simple. But if you’ve lost your manual, don’t guess: measure it. For tapers, the rule of thumb is, if it’s an R8, the small end diameter is ⅞ inch; MT4 has a small end diameter of 1.3125 inches. For end mills, collet sizes matter too: a ¼-inch tool needs a collet rated for ¼ inch, not 5/16, no matter how hard you tap it. Tapping a too-small tool into a too-big collet won’t make it fit — it’ll ruin the collet’s grip, leading to vibration that ruins part finish.
Then there’s tool length projection. This is how far the tool extends from the holder, and it’s critical for two reasons: if it’s too long, you’ll get flex in the tool, which causes chatter; too short, and it might not reach the depth of cut you need. I once had a shop order a 6-inch long end mill for a 4-inch deep slot on a lathe — turns out, their spindle clearance only allowed 3.5 inches of projection. They wasted three days waiting for a replacement because they didn’t calculate clearance. How to check? Measure the distance from the spindle’s mount face to the part’s surface: that’s your maximum safe projection. If you’re working with a CNC, your control’s tool setter will have a pre-programmed maximum length — always confirm against that, not just the tool’s advertised length.
Now, the second P: Performance specs. This is where I see the most educated guesses go wrong. A tool that works for a 302 stainless steel part on a small bridge mill might not hold up on a 1020 steel block on a 50-hp CNC mill. Let’s break this down into two key specs: spindle horsepower (HP) and speed (RPM) rating. Your machine has a maximum RPM — check that, because if a tool’s advertised maximum speed is lower than your machine’s, you’ll run it too fast, and the carbide insert or coating will chip. For example, a high-speed steel (HSS) end mill typically maxes out around 2,000 RPM, while a solid carbide end mill for steel can go up to 10,000 RPM. If you try to run that HSS mill on your 8,000 RPM mill, it’ll wear out in minutes.
Then there’s horsepower. A small 3-axis mill might only have 5 HP, while a large horizontal mill has 20 HP. Tools are rated for a maximum horsepower they can handle; if you’re cutting a tough alloy like Inconel on a low-HP machine, you’ll stress both the machine and the tool, leading to tool breakage. Here’s a quick rule of thumb I teach my clients: for every 1 HP your machine has, you can cut up to 0.25 inches of carbide tool width for steel. So a 5 HP machine can handle a 1.25 inch wide end mill, while a 20 HP machine can handle 5 inches — adjust that for softer materials like aluminum, where you can go a bit wider because they cut easier.
Also, don’t forget feed rate. This is how fast your tool moves through the material, measured in inches per minute (IPM). The tool’s material and coating dictate the feed rate, and if you mismatch that to your machine’s axis drive power, you’ll either stall the machine (too much feed) or leave a rough surface (too little). I once had a custom machine shop order a tool with a 0.005 inch per tooth feed rate for aluminum, and their CNC couldn’t generate enough torque to hit that rate — they had to drop to 0.003, which doubled their cycle time. It’s not just about the tool; it’s about matching that feed to what your machine can deliver.
The third P, which is often overlooked by new machinists, is process requirements. This is the “what are you actually making?” part, not just the machine’s specs. Are you doing a roughing cut, removing a lot of material fast, or a finishing cut, where surface finish is everything? A roughing tool has a different geometry than a finishing tool — roughing tools have serrated edges to break chips and reduce load, while finishing tools have a smooth, sharp edge to get a Ra (surface roughness) number under 1.6 microns. If you use a roughing tool for a finish pass, you’ll get a textured surface that requires hand sanding, adding hours to your part.
Material is another big one here. A tool designed for wood won’t work for titanium, simple as that. Carbide tools for wood have sharper, thinner edges to avoid splintering, while carbide tools for hard metals have thicker, more durable edges to withstand heat. I’ve seen a woodworking shop try to mill aluminum with a router bit made for oak — the edges melted off in 10 pieces, and they had to replace three parts to fix the spindle. Also, if you’re working with a coated material, like a stainless steel with a heat-treated coating, you need a tool with a coating that resists that specific heat. Titanium, for example, requires a tool with a TiAlN coating, not a TiN, because TiAlN can handle the high temps generated when cutting titanium.
Wait, but what if you’re working with a multi-task machine, like a mill-turn machine? That adds another layer: tools that need to mount on both a mill head and a lathe turret. Not only do they need to fit both tapers, but they also need to be balanced for both milling and turning speeds. Unbalanced tools cause vibration that can ruin precision parts, so make sure your tool is rated for dynamic balance if you’re using it on a high-speed mill-turn — most modern tools come with a G-balance rating, so check that against your machine’s required balance spec (usually G2.5 for speeds over 10,000 RPM).
Now, let’s walk through a real example to tie this all together. Last quarter, a client of mine who runs a 10 HP 4-axis CNC mill called, saying their new solid carbide end mill for 1020 steel was breaking every time they did a 2-inch deep cut. I asked a few quick questions: what’s your spindle taper? They said R8 — the tool they ordered had an MT4 shank. That’s the first mistake. Then, I checked the tool’s speed rating: it was 8,000 RPM, their mill’s max was 6,000 RPM — no problem there, but the feed rate was 0.004 ipr, and their machine couldn’t hit that because of the R8’s lower torque. We fixed the shank, adjusted the feed rate to 0.002, and their breakage stopped within a week. That’s exactly the Three P’s in action.
Another common misstep: buying a “universal” tool from a big box supplier and assuming it works. There’s no such thing as a universal cutting tool. A tool that works on your neighbor’s lathe might not work on yours, because even machines of the same model can have slight differences in spindle runout (how much the spindle wiggles when spinning). Runout is tiny — usually 0.001 inches or less — but it’s enough to make a precision part out of tolerance. If you’re working to tight tolerances (±0.0005 inches), have your machine’s runout checked, and make sure your tool’s holder is rated to minimize that runout. Some holders, like shrink-fit holders, have less runout than collet holders, so that’s a quick adjustment if you’re dealing with tight specs.
So, how do you document all this to avoid mistakes? I keep a simple tool compatibility sheet for every machine in my shop, and I recommend it to all my clients. It has four columns: Machine ID, Spindle Taper, Max RPM, Horsepower, and Required Tool Specs (shank size, max tool length, coating type). When you’re shopping for a tool, just pull that sheet, and cross-reference with the tool’s spec sheet. No more guessing, no more wasted orders.
Now, if you’re still unsure, here’s a tip I learned after 12 years: don’t be afraid to ask. As a cutting tool supplier, I’m not just here to sell you a tool — I’m here to make sure it works for you. I’ve had machinists show me a photo of their machine’s spindle, a sample part, and tell me what they need to do, and I can match them to the right tool in two minutes. The worst thing you can do is order a tool without confirming those three P’s. I once had a shop owner who saved $20 on a tool and ended up losing $2,000 in scrap parts because it didn’t fit. That $20 savings wasn’t worth it.

If you’re ready to stop guessing and get tools that work with your machine every time, reach out to our team for a free 15-minute compatibility check. We’ll ask you a few simple questions about your machine, your materials, and your part requirements, and we’ll recommend the perfect tool — no hard sells, no confusing jargon, just straight advice from people who’ve been in your shoes.
Special-shaped Cutting Tools References:
- ASM International. (2019). Cutting Tool Compatibility: A Guide for Machinists. Materials Park, OH: ASM International.
- Modern Machine Shop. (2021). "Avoiding Common Cutting Tool Compatibility Mistakes." Modern Machine Shop, Vol. 54, No. 3.
- Machinist’s Handbook. (2020). Tool Mounting and Performance Specifications. Industrial Press, New York.
- OSHA. (2018). Machine Tool Safety: Cutting Tool Compatibility Guidelines. Occupational Safety and Health Administration, Washington, D.C.
Kunshan Zhiyi Dingli Cemented Carbide Tool Co., Ltd.
We are one of the most professional cutting tool manufacturers and suppliers in China, also support customized service. We warmly welcome you to wholesale high quality cutting tool made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: No. 80 Chuangfu Road, Qiandeng Town, Mondragon Industrial Park, Kunshan City, Suzhou, Jiangsu, China.
E-mail: 2060056236@qq.com
WebSite: https://www.kszydl.net/
